
Quality
Material, inspection and the document package
Material, heat treatment, coating and inspection are taken from the drawing and the project specification. The methods listed here are capabilities that can be included; they are not applied automatically to every part family.
Materials commonly specified
| Family | Grades reviewed to the drawing | Notes |
|---|---|---|
| Carbon and alloy steels | 1010, 1018, 10B21, 35CrMo / 42CrMo, SCM435, and S355J2 / S355J2+N for certain fittings | Other grades reviewed by enquiry |
| Stainless steels | 304 (A2), 316 (A4), and 410 where relevant | Condition and magnetism as specified |
| Copper and copper alloys | Brass and other copper alloys, including CW614N, CuZn39Pb3, CuZn40Pb2 and CuZn36Pb2 when specified | Typical finish for these fitting parts is natural / unplated, unless the print states otherwise |
| Aluminium | EN AW-6060 T6 (AlMgSi), and other grades when specified | Used for example on membrane-housing stage parts; condition and finish follow the print |
Mechanical values, temper and any restriction on leaded alloys are taken from the print. Fittings and valve components describes how these grades are used on gas-equipment parts.
Property class and heat treatment
Bolt and screw property classes including 8.8, 10.9 and 12.9, and nut grades 8, 10 and 12, can be produced after heat treatment when those classes are specified.
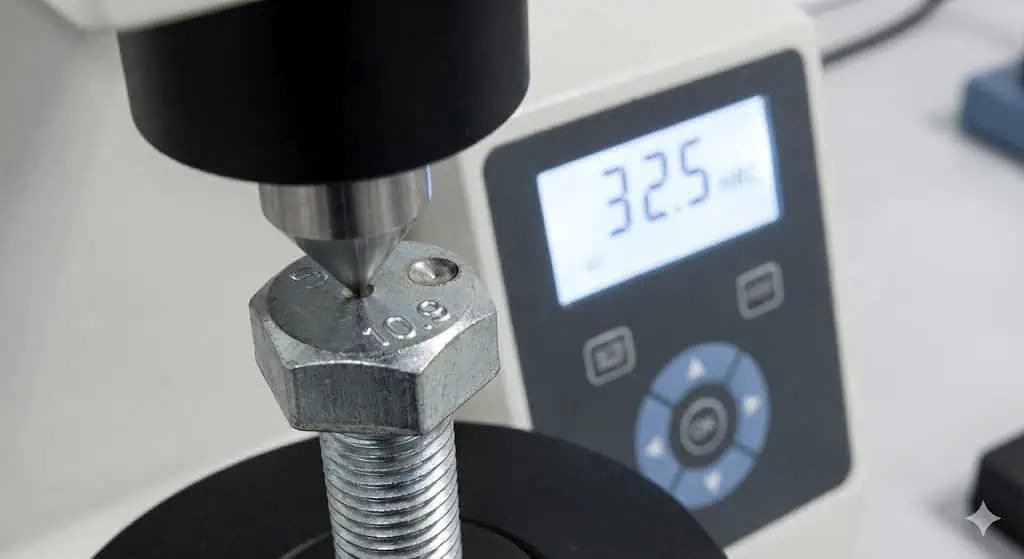
Heat-treatment routes include quench and temper to the stated property class, carburizing, and annealing, as applicable to the grade and the drawing. Mechanical evidence — hardness, proof load, tensile properties — is added to the inspection plan when the order requires it.
Coatings and friction
Finishes that can be reviewed include trivalent zinc (RoHS), zinc-nickel, zinc-flake systems, passivation, and a wax or topcoat used to hold a specified friction window. Carbon-steel fitting parts are often zinc plated when that is specified; many brass and copper-alloy fitting parts are supplied in a natural, unplated finish.
Zinc-flake systems such as Geomet or Dacromet are cited as examples of coating types, not as SUNHY-owned brands, and not as a guaranteed salt-spray result on every part. Corrosion-test hours are treated as a typical range or process target for the specified system, not as a guarantee on every lot.
High-strength parts and hydrogen embrittlement
Zinc-flake coatings are non-electrolytic, which is often a reason for reviewing them on high-strength parts. Pretreatment, any electrolytic step, baking and the overall process still require review when property class 10.9, 12.9 or an equivalent high-strength condition is specified. The method is agreed in the quotation; it is not assumed.
Inspection, sorting and cleanliness
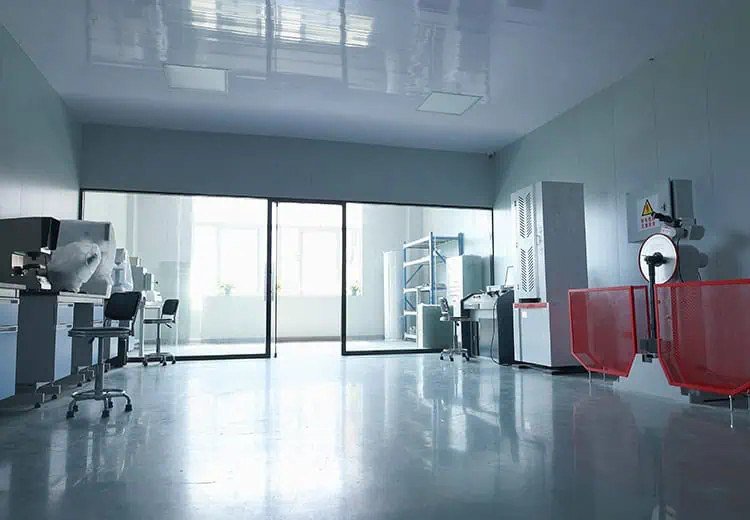
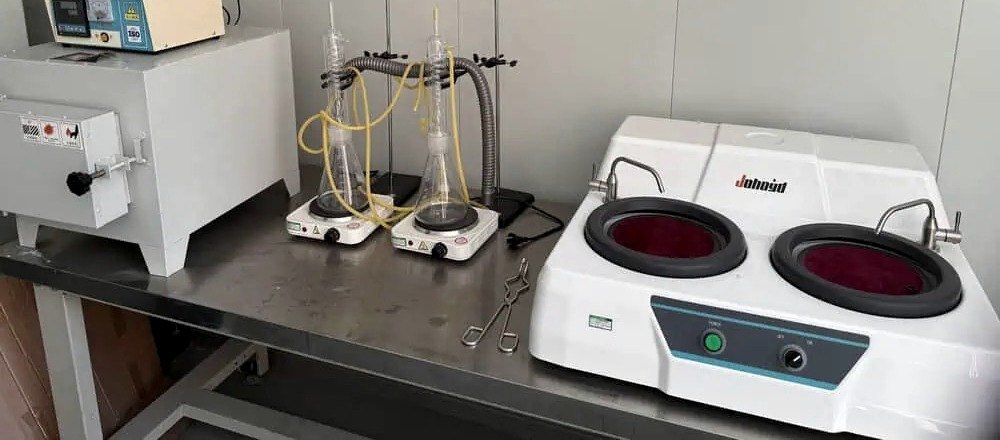
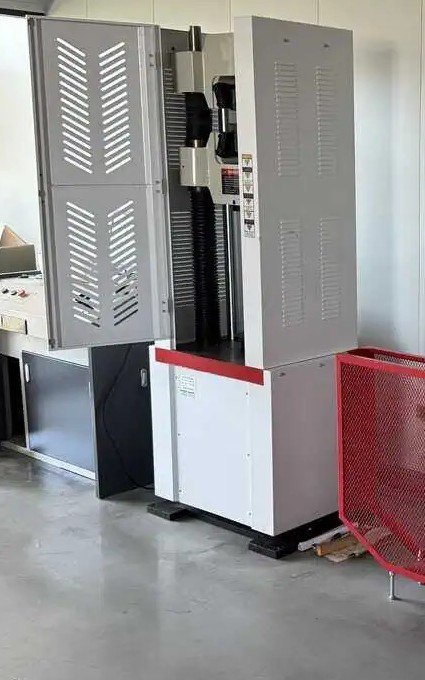
Material and mechanical
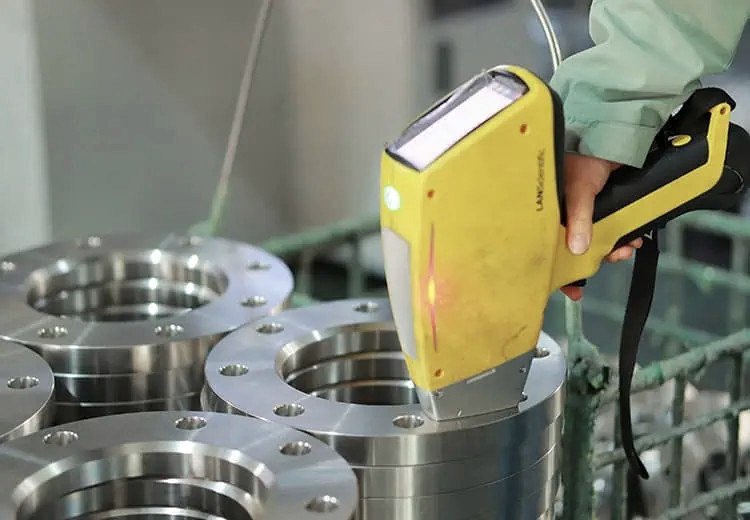
- In-house spectrometer / PMI
- Hardness (HRC / HV)
- Proof load and torque testing
- Other mechanical tests as specified
Dimensional and thread
- Go / no-go thread gauging
- Critical dimensions to the drawing
- Concentricity and runout, as required
- Gauging after coating, when specified
Sorting and cleanliness
- High-speed optical, camera or laser sorting against an agreed plan
- Automated ultrasonic cleaning, where the route includes it
- Visual or attribute checks defined by the part
Optical sorting and PPM figures
Optical sorting can be applied to a part family when the enquiry calls for it and a sorting plan is agreed. Programme targets such as below 50 PPM or 0-PPM may be discussed. Those figures are targets, not guarantees, and they do not mean that every part family is 100% sorted.
Documents, PPAP and IMDS
EN 10204 3.1 inspection documents can be supplied on request and are confirmed per order.
PPAP submission and IMDS entry are reviewed for the particular part. The level, the required evidence, and whether IMDS entry is included are stated in the quotation. They are not an automatic or already-certified capability on every item.
Quality-system reference
ISO 9001 may be referenced as a quality-system framework. The legal entity, manufacturing site, product scope and validity are confirmed for the order before any certificate is cited.
A quality-system certificate is not a substitute for a customer-required automotive quality-management scheme, and it is not presented here as product approval.
Packaging, labelling and Incoterms
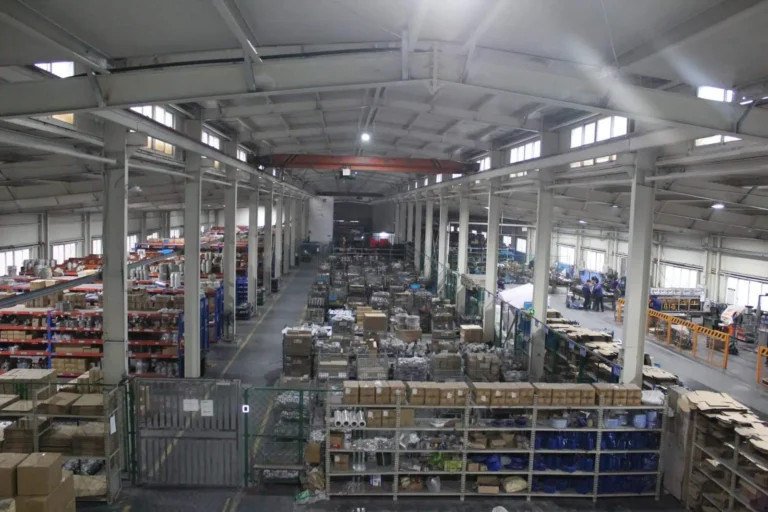
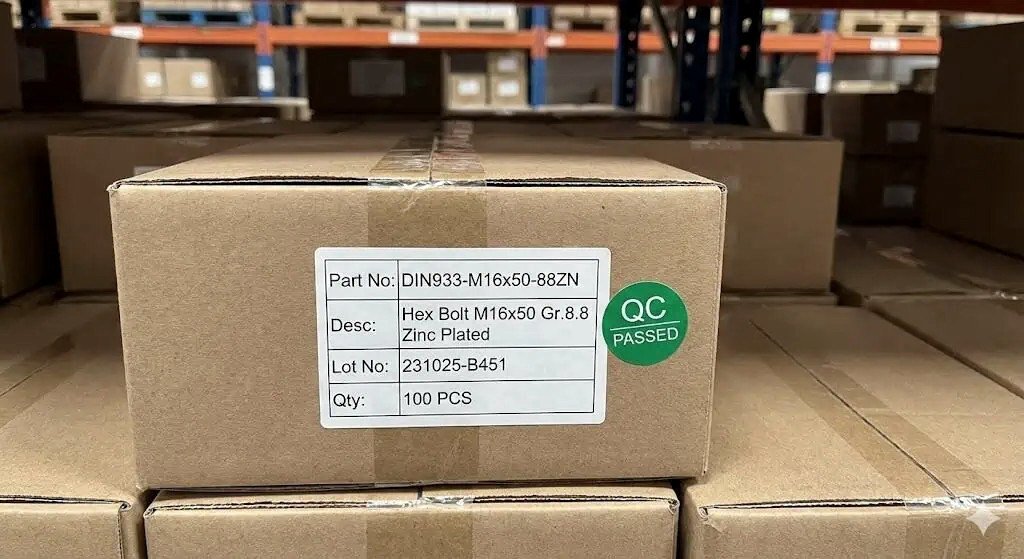
Unit pack, carton quantities, label fields, language and any barcode or 2D-code requirement should be stated in the RFQ. Lot identification on the pack is used so that a shipment can be traced back to the production lot and to the incoming material, in line with the agreed route.
Shipments can be quoted under FOB, CIF or DDP terms. The applicable Incoterm, the named place, and the scope of DDP — including how duties, taxes and delivery to a given site are handled — depend on the agreed quotation and the destination. They are not a standing door-to-door commitment independent of the order.
State the quality requirements with the print.
Unspecified points will be flagged before production rather than assumed. The quotation confirms the inspection and document package for that part.